Introduction
Home repair gets frustrating when a job depends on doing the same thing exactly the same way more than once. The first attempt looks fine, the second drifts a little, and by the third the error is visible. That drift is rarely about effort. It is about having no fixed reference, so every repetition becomes a fresh guess, and a small early error is copied across the whole job.
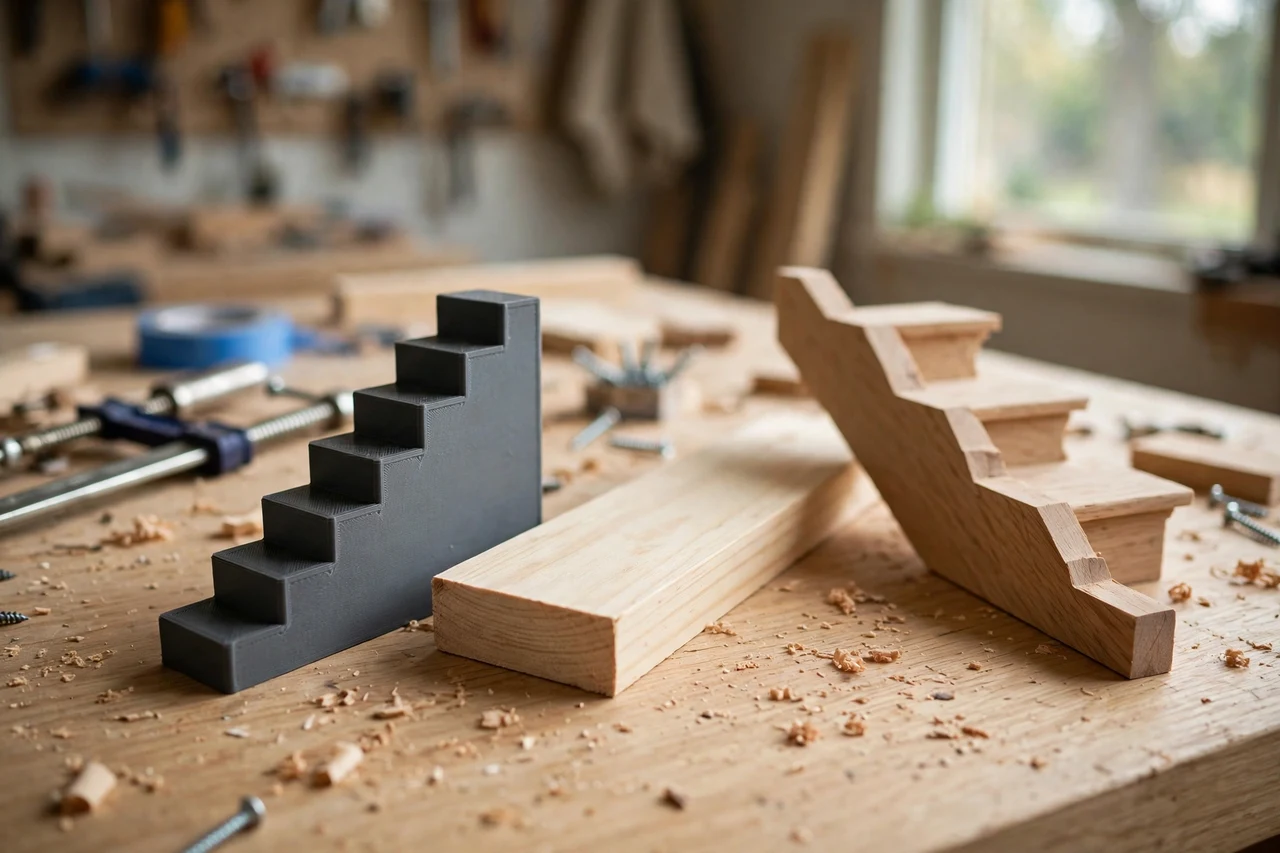
A 3D printed stair riser height gauge removes that guesswork. Its job is to give you a physical reference you can press, clamp, or register against the workpiece while you are checking stair riser heights for an even climb, and it does so by fixing one measurement or angle so you do not have to re-establish it each time. Once the reference is set, repeating the job means repeating the setup rather than re-measuring from scratch. The classic failure this kind of jig prevents is risers checked individually, hiding one rise that is taller than the rest, and a fixed reference is the simplest cure for it.
That repeatability matters most where several parts must agree. A run of matching pieces is compared piece by piece, and any drift shows as a step or a gap. A printed reference turns a measurement you must remember into a shape you can feel, and it still holds the setup when you return to the job days later.
This guide covers the whole process in an original design of your own: what you need, the design choices that matter, how to print and test the part, and how to use it on a real repair. The key measurement throughout is riser height, tread depth, and stringer angle, so measure that on your own materials before you model anything. Treat the printed part honestly: it is a guide, holder, or light-duty aid, never a structural or load-bearing part and never a substitute for rated hardware, and never for gas, pressure, live electrical, or child-safety use. Two companion projects worth a look are 3D Printed Stair Handrail Post Spacing Gauge and 3D Printed Cabinet Door Hinge Boring Template, which pair naturally with this guide because they solve the same kind of repeatability problem in a different corner of the workshop.
What You Need
You do not need an exotic printer for this project. Most home printers can make a useful stair riser height gauge in a single print, and the supporting tools are probably already in your workshop. Gather everything before you start, and keep the real workpiece close at hand for test fitting.
Materials and tools
- A home 3D printer with a build area large enough for the part laid flat
- PETG filament for a tougher keeper, or PLA for a first test version
- The real workpiece the stair riser height gauge must match, for test fitting: stair risers and stringers
- A tape measure or calipers, a pencil or fine marker, and a small clamp
- Sandpaper or a small file, a screwdriver, and the hand tools the job normally needs
- Safety glasses and work gloves for the repair work itself, used as the task requires
PETG is the better long-term choice because it flexes rather than cracking and copes better with a warm garage. PLA is good for checking fit. Print a test first either way: a short check print is cheaper than a failed repair.
Suggested print settings
- Layer height: 0.20 mm balances speed and accuracy; 0.16 mm for fine edges.
- Walls: At least 3 to 4 perimeters, since reference edges do the real work.
- Infill: 30 to 50 percent, grid or gyroid, so the part resists flexing when clamped.
- Top and bottom layers: 4 or more, keeping contact faces smooth.
- Orientation: Print flat, main reference face down, for the flattest surface.
- Supports: A well-designed version needs none, though a tall fence may need a small brim.
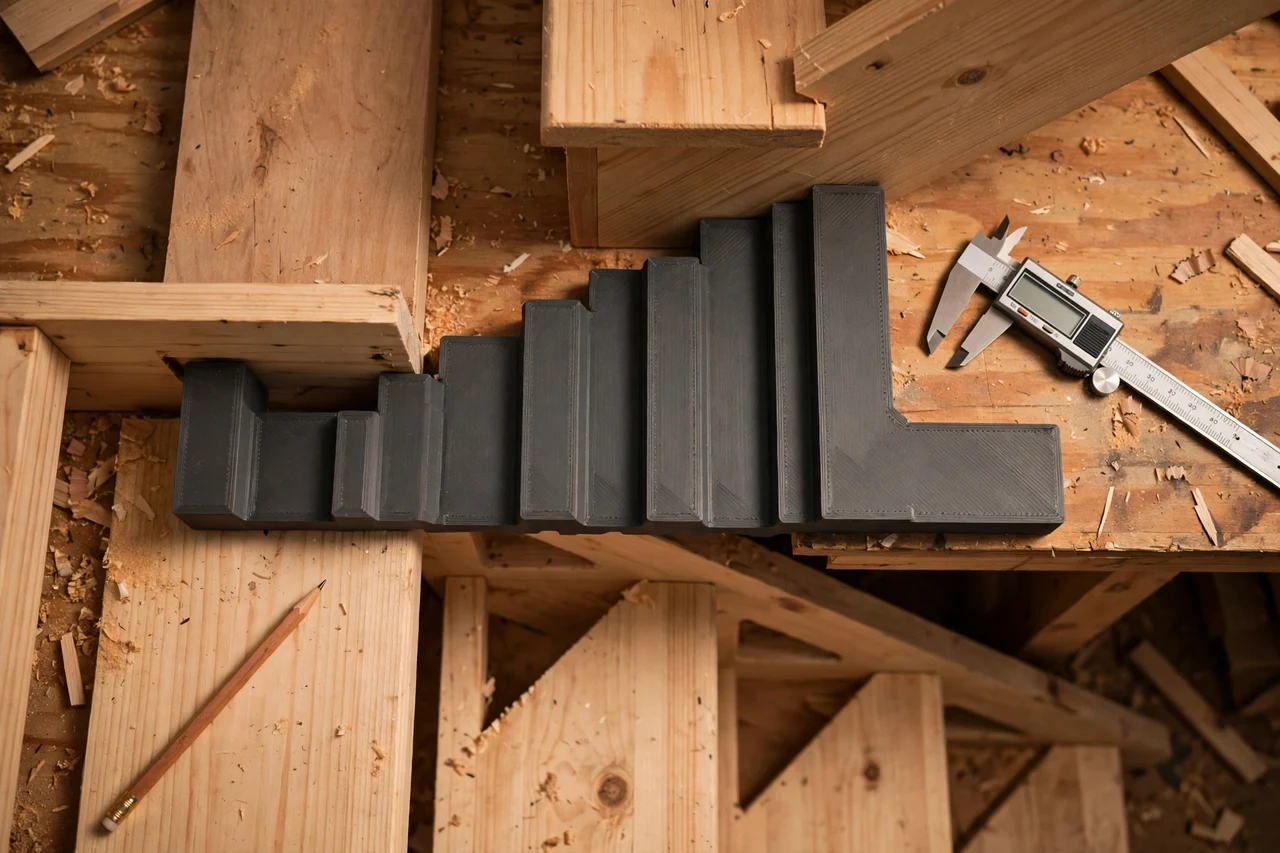
Design Considerations
A good stair riser height gauge is not complicated, but a few design decisions decide whether it feels precise or sloppy. Work through these before a final print, testing each against the real workpiece.
1. Fit and registration
Every useful guide has one face or edge that registers against something real: a board edge, a tool body, or a flat surface. Make that surface generous, square, and clean. A narrow or rounded reference lets the part rock, and every mark made from it inherits that movement. Aim for 8 to 12 mm of solid contact.
2. Clearance and sizing
Measure the actual item in your hand, not a nominal size from a listing. For this project that means checking riser height, tread depth, and stringer angle on your own materials, because brands and batches vary, and a few tenths of a millimetre matter when a guide is supposed to locate something repeatably. Allow about 0.3 to 0.5 mm of clearance per side on any slip fit: tight enough to locate firmly, loose enough to remove without force. If a fitting varies between brands, consider a flexible clip or short slots rather than one rigid hole, so one printed part covers a small range instead of needing a reprint for every variant.
3. Strength where it matters
Printed plastic is strong in some directions and weak in others, so orient the part so clamping pressure acts across the layers rather than peeling them apart. Thicken areas around holes, clips, and fences, and add a small fillet where a fence meets the base so it does not snap at the joint. Generous walls and infill matter more than exotic filament, and a part that flexes under a clamp has failed its main job, however neat it looks.
4. Handling and repeatability
Add small features that make a guide pleasant to reuse: rounded outer corners, a finger notch where a part must be lifted out, and a mark showing which way up it goes. If you print several sizes, mark each with a paint pen so you grab the right one without test fitting. Store it with the tools for this job.
Step-by-Step: Making and Printing It
- Measure the real thing. Record riser height, tread depth, and stringer angle, including any thickness, offset, or position the guide must match, and write the numbers down rather than trusting memory.
- Sketch the part on paper. Note the registration face, the working features, and where your hand or a clamp will sit, and check the sketch against the workpiece before modelling.
- Model it simply. Start with a flat plate or body, then add the fence, slot, clip, or recess it needs, and nothing extra.
- Print a test version. Use inexpensive filament and check the fit against the real workpiece before anything else.
- Clean it up. Remove stringing, clear holes by hand, and lightly sand any reference face that feels rough.
- Adjust in small steps. If a fit is tight, open it by 0.2 mm and reprint; if loose, close it the same amount. Change one dimension at a time so you know what fixed it.
- Print the keeper. Use PETG if the part will live in the workshop with the same settings that passed the test.
- Label it. Mark the size or purpose on top so the part is easy to identify on a busy bench, and note the key measurement on the label if the jig is size-specific.
Do not rush the test fit: it catches errors before they reach the real job.
Step-by-Step: Using It on a Real Repair
- Set up a clean, flat workspace. Clear the bench, lay the workpiece on a padded surface, and gather the tools for the job.
- Check the fit on scrap first. Run through the step on an offcut of the same material, checking riser height, tread depth, and stringer angle as you go.
- Position the stair riser height gauge carefully. Press its registration face fully against its reference, with no gap or rocking.
- Clamp or hold it firmly. A guide that moves mid-job is worse than no guide at all; check the clamp before you start.
- Make your marks or cuts slowly. Let the guide do the locating work; do not force the tool against it.
- Remove the part and inspect. Check the mark, cut, or fit before committing to the next step of the repair, and measure it rather than eyeballing it.
- Repeat from the same setup. Re-seat the guide the same way rather than re-measuring from the far end, so every repetition inherits the same reference.
- Finish the repair normally. Fit and fasten the piece, then check alignment and gaps before calling it done.
- Clean and store the part. Brush off dust and debris so the next job starts from a clean reference face, and put the jig back with the tools for this job.
Work slowly on the first real use; if a result looks wrong, stop and re-seat the guide rather than repeating the error across every remaining piece.
Tips for Better Results
- Test on scrap when you change material. A setting that worked on one piece may not suit the next.
- Keep reference faces clean. One trapped chip is enough to throw a mark off, so brush the face before every seating.
- Mark the orientation on the part. A simple arrow stops you flipping it.
- Use the same guide for matching sides. Pairs made from one setup agree better than pairs measured separately.
- Check one result before repeating it. Confirm the first piece against the real assembly.
Common Mistakes to Avoid
- Designing from a photograph instead of the real item. Lookalikes often differ by a few millimetres.
- Making fits too tight. A part that must be forced on will flex or crack and will not sit the same way twice.
- Skipping the clamp or the scrap test. Both feel like delays, and both separate a neat result from a frustrating one.
- Printing too light. Thin walls and low infill flex under pressure.
- Ignoring the job-specific trap: risers checked individually, hiding one rise that is taller than the rest. Check for it explicitly on the first piece.
- Forgetting the honest limits. Printed parts are guides, holders, and light-duty aids only. Never use one as a structural or load-bearing part, or a substitute for rated hardware, and never for gas, pressure, live electrical, or child-safety use.
Care, Storage, and When to Choose an Alternative
Brush off dust after use, store the part flat where it will not be crushed, and keep PLA away from hot cars and direct sun. Check the reference edge before each reuse, and reprint if it is nicked, warped, or no longer sits flat.
Sometimes another material is better. If you use the guide daily or need tolerances a home printer cannot hold, a metal or commercial version will outlast plastic. For occasional repairs, a printed guide is faster, easy to replace, and accurate enough within its limits.
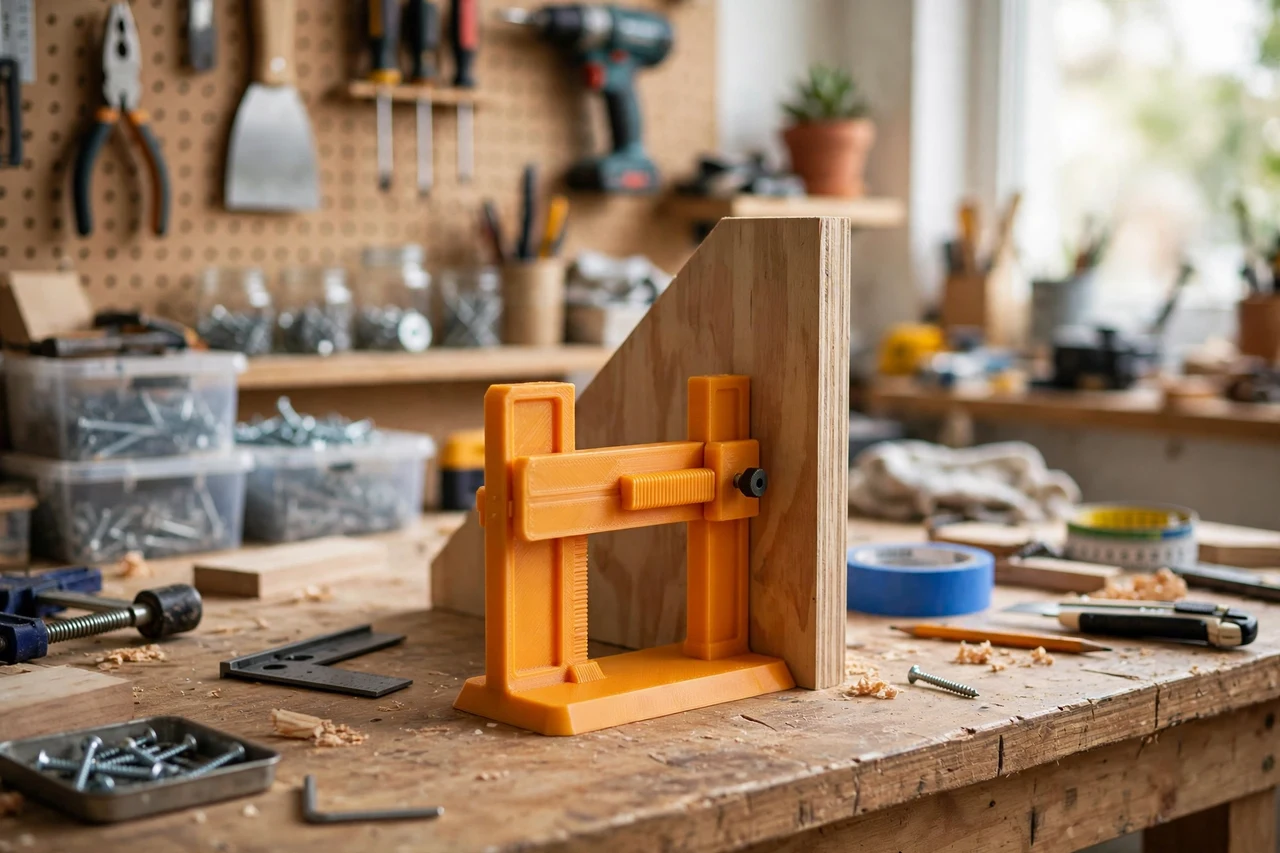
FAQ
What material should I print a stair riser height gauge from?
PETG is the best default for a keeper because it handles drops, clamping, and warm workshops better than PLA. PLA is fine for test prints and light indoor use. Generous walls and infill matter more than filament brand.
Will one printed stair riser height gauge fit every version of this job?
Not always. Sizes vary between brands, so measure your own workpiece and size the part to it, especially riser height, tread depth, and stringer angle. A very different size deserves its own version.
Can I use this printed guide for heavier work than described here?
No. Printed parts here are guides, holders, and light-duty aids only. They are never structural or load-bearing, never a substitute for rated hardware, and never suitable for gas, pressure, live electrical, or child-safety use. If a job needs real strength, use the proper metal or commercial equivalent.
My printed stair riser height gauge fits too tightly or too loosely. What should I change?
Adjust clearance by 0.2 mm at a time and reprint a test section if you can, rather than changing several things at once. Check for stringing first, since cleanup often fixes a tight fit.
Conclusion
A repeatable repair is rarely about working harder. It is about working from the same reference every time, and that is exactly what a 3D printed stair riser height gauge gives you. With a careful measurement, a simple model, and a test print, a fiddly step becomes a calm routine.
Print one to match the tools you already own, keep it with the kit for that job, and the next repair of this kind becomes shorter and neater. Good companions are 3D Printed Stair Handrail Post Spacing Gauge and 3D Printed Cabinet Door Hinge Boring Template, and the full set continues from there.