Introduction
Concealed hinges — the cup hinges inside nearly every modern kitchen cabinet — look effortless when they work. The door closes softly, sits flush, and adjusts with a turn of a screw. Getting there, though, depends on one unforgiving step: boring a 35 mm cup hole in exactly the right place, at exactly the right depth, square to the door.
Freehand that hole and the problems stack up fast. A Forstner bit that starts a fraction off center leaves a cup the hinge cannot sit flat in. A hole drilled a millimeter too deep breaks through a thin door skin. A hole that wanders toward the edge leaves too little wood for the hinge screws to grip.
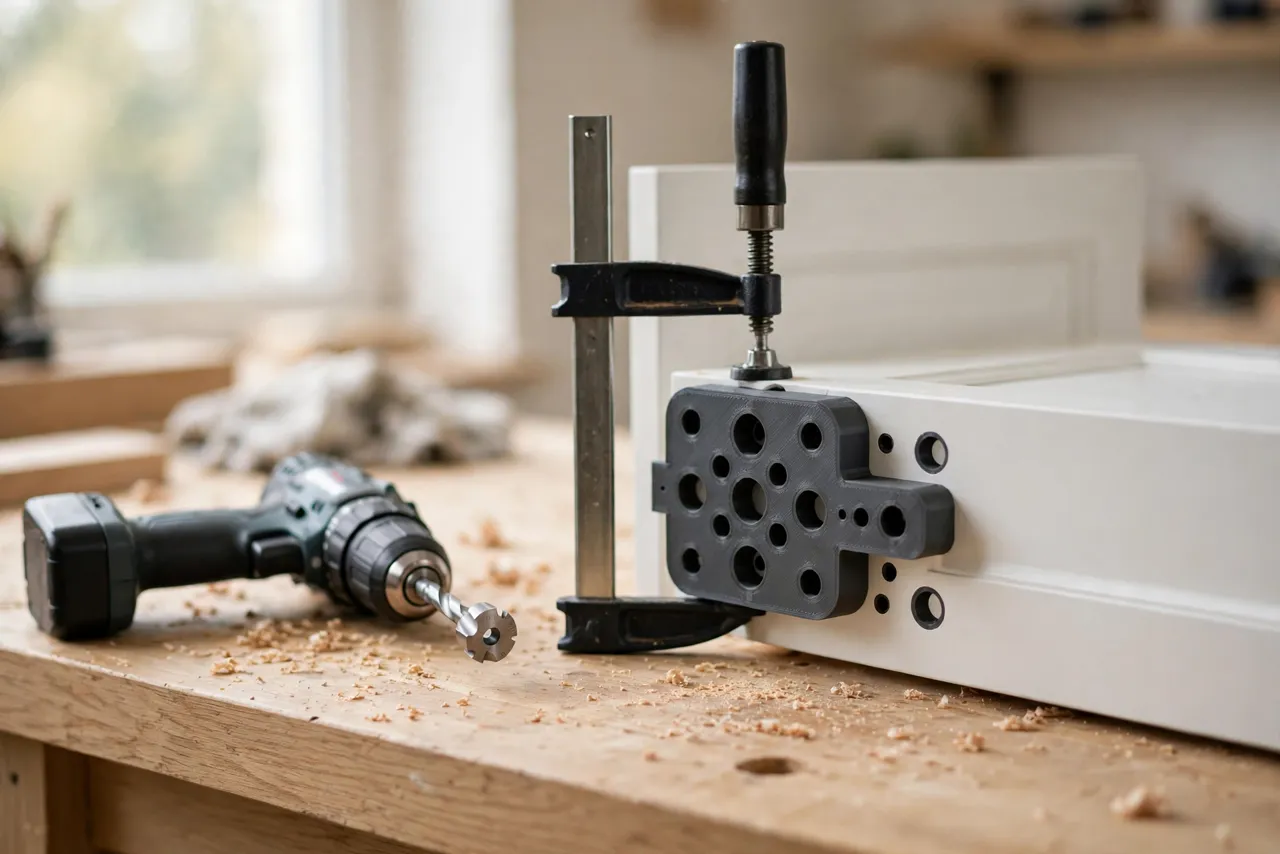
A 3D printed concealed hinge cup drilling template removes the guesswork. It clamps to the door edge, centers the 35 mm cup on your chosen setback, and guides the bit straight down to a controlled depth. Print it once for the hinges you own, and every door in a run comes out the same.
Think of the template as a layout and drilling aid only — it does not carry the door’s weight, and it never replaces checking your hinge maker’s own setback and depth figures.
What You Need
The template is a compact, flat part with a round guide hole and a fence. It fits easily on most home printers.
Materials and tools
- A home 3D printer with a build area of roughly 150 mm in at least one direction
- PETG filament for a durable template, or PLA for a first test version
- A 35 mm Forstner bit and a drill or drill press, plus a depth stop or tape flag
- The actual concealed hinge you plan to install, plus its screws, for test fitting
- A cabinet door to measure, a tape measure or calipers, and a pencil
- A small clamp, sandpaper or a small file, and scrap board of the same thickness
PETG is the better keeper: it handles clamping and the vibration of drilling without cracking. PLA works for a first version — just keep it out of direct heat.
Suggested print settings
- Layer height: 0.20 mm balances speed and accuracy; 0.16 mm if the guide hole looks rough.
- Walls: 4 to 5 perimeters — the guide ring takes the most wear.
- Infill: 40 to 50 percent, grid or gyroid, so the template stays rigid under a clamp.
- Top and bottom layers: 4 or more, for a smooth face against the door.
- Orientation: Print flat, door-facing side down, for the flattest reference surface.
- Supports: A well-designed template needs none.
Print one test version first and check the cup fit on scrap before drilling a real door.
Design Considerations
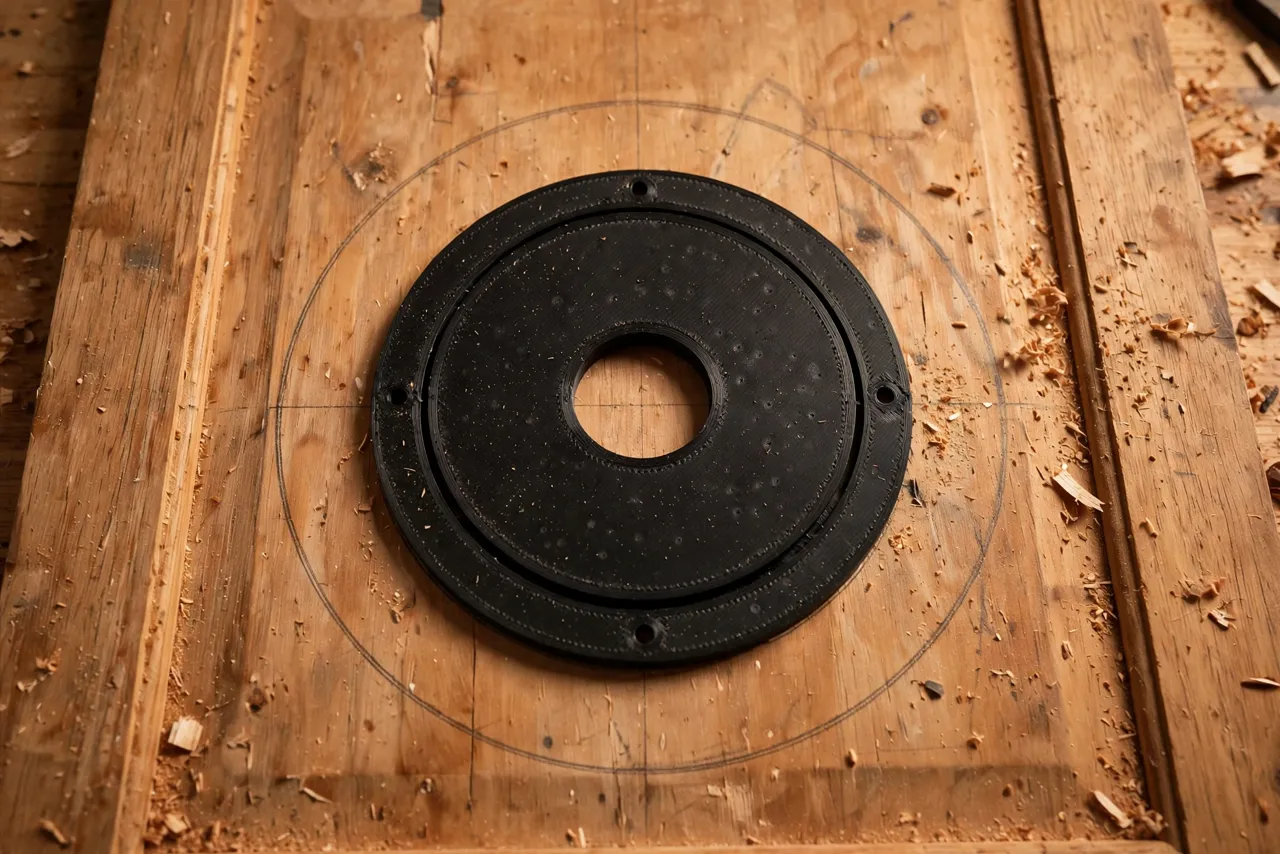
You can model this template in any basic CAD program. It is essentially a flat plate with a fence, a round guide hole, and small screw-mark holes.
1. The reference fence
The fence hooks over the door edge and sets the cup’s distance from that edge — the setback — every time. Common setbacks put the cup center 21 to 23 mm from the edge, but always check your hinge’s own specification. Give the fence 10 to 15 mm of contact and keep its inside corner square. A rounded corner lets the template rock, and every cup inherits that error.
2. The 35 mm guide hole
The guide hole centers the Forstner bit. Size it for a snug slip fit around the bit’s outer rim — about 35.5 mm works well for most 35 mm bits, but measure your actual bit, since nominal sizes vary. The hole wall should be at least 4 mm tall so the bit stays square through the first critical millimeters of the cut. Some makers add a thin sacrificial ring that can be replaced when the hole wears.
3. Screw-hole marks
Through the plate, add small holes aligned with the hinge’s two screw positions. These transfer the screw centers with a pencil or awl after the cup is bored. Position them from your actual hinge, not from a diagram — screw spacing differs between hinge brands.
4. Depth control
The template itself does not set depth; your drill does. But a good design helps: add a flat top surface the drill’s depth stop can reference, and print a small depth gauge block as a companion piece — a stepped block marked at common cup depths (usually 11 to 13 mm) that you hold against the bit to set the stop. Test depth on scrap first, every time, because door thickness and hinge cup depth must leave solid wood behind the cup.
Step-by-Step: Printing and Fitting the Template
- Measure your hinge — cup diameter, cup depth, screw spacing, and the maker’s setback figure.
- Measure your bit with calipers; do not trust the printed size alone.
- Measure your door thickness at the hinge location.
- Model the plate, roughly 150 mm long, 90 mm wide, and 6 mm thick, with fence, guide hole, and screw marks.
- Print a test fit. The Forstner bit should slide through the guide hole without binding.
- Clean it up. Remove stringing, sand the fence face, and clear the screw-mark holes.
- Bore a test cup in scrap and drop the hinge in. It should sit flat, flush, and centered.
- Adjust if needed. Cup off-center? Shift the guide hole by the error and reprint. Small iterations are normal.
- Print the keeper in PETG if your test was PLA, using the same file.
Never skip the scrap test. A door with a misplaced cup is very hard to repair invisibly.
Step-by-Step: Using the Template on a Cabinet Door
- Remove the door and lay it flat, inside face up, on a padded surface.
- Decide the hinge positions. Measure from the top and bottom of the door to each cup center and make a light pencil tick on the edge. Do this once, carefully.
- Seat the template. Press the fence against the door edge and slide the template until its center mark lines up with your tick.
- Clamp it firmly. Check the fence is flush along its whole length, with no chip trapped underneath.
- Set your depth stop using the gauge block or a tape flag, verified against your scrap test.
- Bore the cup at moderate speed, steady pressure, backing out once or twice to clear chips. Let the bit cut; do not force it.
- Remove the template and mark the screw holes through the guide holes, then drill small pilots.
- Fit the hinge, driving screws snugly without stripping the holes.
- Repeat for the second hinge, then hang the door and adjust the hinge screws until gaps are even.
Work slowly on the first door. By the second, the routine feels automatic — and that consistency keeps a whole run of cabinets looking even.
Tips for Better Results
- Use a sharp Forstner bit. A dull bit wanders, burns, and tears the cup rim.
- Clamp, don’t hold. A hand-held template shifts during the cut, however steady your hands feel.
- Clear chips often. Packed chips overheat the bit and push it off line.
- Test depth on scrap of the same thickness. Door skins vary, and a millimeter matters here.
- Mark top and bottom on the template. A simple arrow stops you flipping it and offsetting a cup.
Common Mistakes to Avoid
- Designing from a diagram instead of your own hinge. Cup depth and screw spacing differ between brands. Measure the hardware in your hand.
- Making the guide hole too tight. A binding bit tilts and scores the template — and the cup.
- Skipping the depth stop. Eyeballing depth on a Forstner bit is how doors get drilled through.
- Drilling on a bowed or unsupported door. Support the door fully so it cannot flex away from the bit.
- Forgetting handing. Check which edge the hinge belongs on before you bore, not after.
Care, Storage, and When to Choose an Alternative
Brush off dust, store the template flat or hang it from a peg, and keep PLA away from hot cars and radiators. If the guide hole wears oval, reprint — it takes less than an hour.
Sometimes a manufactured jig is better. If you fit concealed hinges all day, work through dozens of doors, or need hardened steel bushings for a self-centering bit, metal will outlast plastic and hold tighter tolerances. For occasional home repairs and matching an odd hinge you already own, a printed template is faster, easy to customize, and accurate enough.
FAQ
Will one template work for every concealed hinge?
Not quite. A template is sized around one cup diameter, setback, and screw pattern. Most kitchen hinges share the 35 mm cup, but setback and screw spacing vary, so a very different hinge deserves its own version — which is cheap and quick to make.
Is PLA strong enough, or do I need PETG?
For marking and light clamping, PLA is strong enough and great for testing fit. PETG is the better keeper because it handles drilling vibration, clamping, and warm workshops better. Either way, generous walls and infill matter more than the name on the spool.
Can I use the template with a drill press instead of a hand drill?
Yes, and a drill press makes depth control easier. Clamp the door to the table, set the press depth stop from your scrap test, and lower the bit steadily. The template still earns its keep by centering the cup and marking the screws.
My hinge rocks in the cup after using the template. What went wrong?
Usually the cup is too shallow, too deep, or slightly off square. Check depth against the hinge maker’s figure, confirm the bit entered square, and re-test on scrap. A hinge that sits proud on one side often means a chip was trapped under the template.
Conclusion
A crooked concealed hinge is usually not a skill problem. It is a centering-and-depth problem, and that is exactly what a simple drilling template solves. With an hour of printing and a few minutes of test boring, 35 mm cups start landing dead center, at the right depth, door after door.
Print one to match the hinges you use most, keep it with your Forstner bit, and the next cabinet door becomes a short, satisfying fix.
For the rest of the door project, you may also enjoy “3D Printed Hinge Jig for Cabinet Doors: Get Perfect Alignment on Every Repair” and “3D Printed Biscuit Joiner Alignment Jig: Cut Slots That Actually Line Up,” which pair naturally with this template for a complete cabinetry setup.